Wrightfield
From a Single Conveyor to a Complete Processing Line
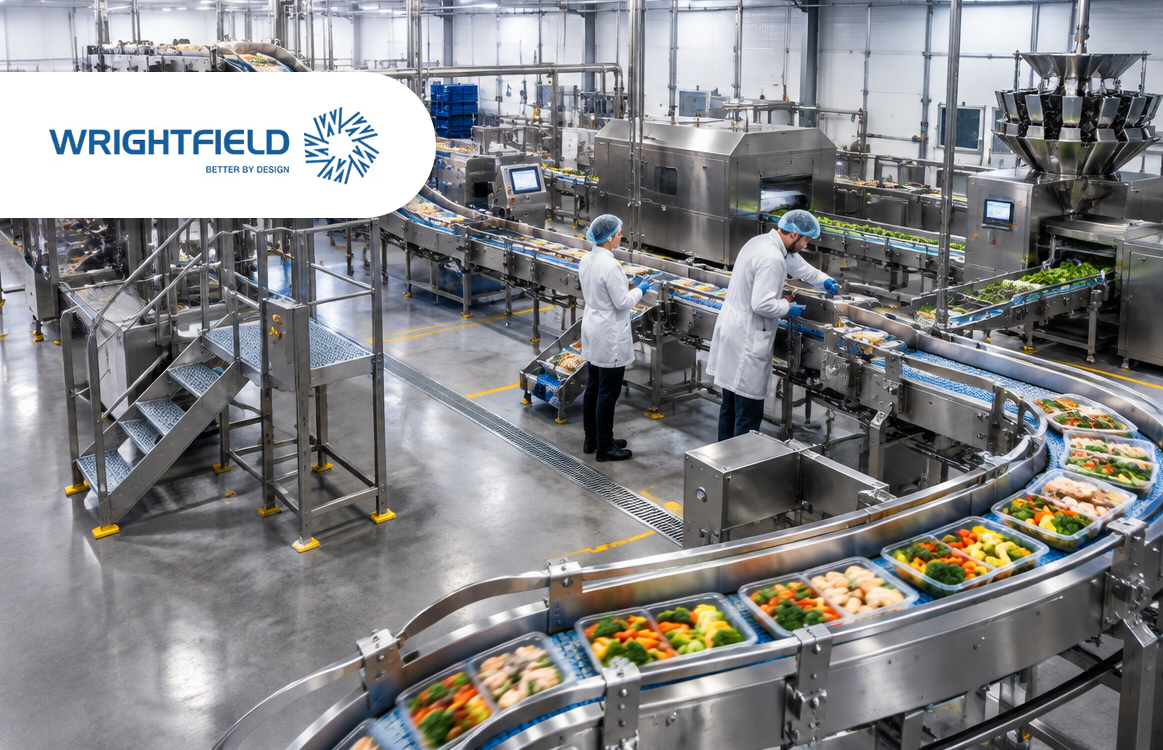
Rather than selling off-the-shelf equipment, Wrightfield designs each system around the specific product, process, factory layout, and hygiene requirements of a given site. That’s backed up by a fairly comprehensive in-house setup: a 40,000 sq ft UK manufacturing facility where the team handles everything from concept, project planning, and 3D design through to precision fabrication, controls integration, installation, and after-sales support. Work includes custom stainless-steel conveyors, structural steelwork and access platforms, automated live bird handling and stunning systems, and full-line integration with existing machinery.
The client base spans small independent food processors through to major multinational brands, and the company also partners with specialist equipment manufacturers, Liftvrac for flightless incline conveying, Turatti for fresh produce processing, MHS for slicing and portioning, and Gamma-Wopla for poultry drawers, bringing in specialist technology where a project calls for it rather than trying to build everything from scratch.
Accreditation-wise, Wrightfield holds EN-1090 certification for structural steelwork, SafeContractor status, Constructionline approval, and Made in Britain membership, verifying its UK manufacturing base. Forty years on from 1985, the company still frames its work the same way it started: solving specific production problems through custom engineering rather than generic equipment, delivered end-to-end by its own in-house team from first site survey through to ongoing servicing and spares.
 Own or work here?
Claim Now!
Claim Now!
Contact with business owner
 Your request has been submitted successfully.
